Fused filament
Extrusion of heated thermoplastic. Useful for prototypes, bench organisation and teaching aids. Intraoral use requires specific materials and processes.
04 — 3D printing
Technologies, resins, slicing, supports, washing, post-curing, safety and clinical validation. The aim is to separate real applicability from commercial promise.
Twelve blocks · open what you need
3D printing is a form of additive manufacturing: the object is built layer by layer from a digital model. In dentistry it became part of the CAD/CAM workflow because it allows intraoral scans, laboratory models and surgical plans to be turned into models, guides, prototypes, occlusal devices, prosthetic bases and polymer restorations.
Consolidation of stereolithography, in which a photosensitive resin is selectively polymerised by light. That principle still underpins SLA, DLP and MSLA/LCD.
Industrial expansion of rapid prototyping and gradual entry into the medical field for anatomical models, guides and planning.
Dental popularisation with intraoral scanners, CAD software, benchtop printers and biocompatible resins.
Broader clinical and laboratory use, but highly dependent on indication, material, equipment, parameters, post-processing and traceability.
How a layer is formed helps explain materials, throughput and limitations. The technology alone does not validate a clinical indication.
Extrusion of heated thermoplastic. Useful for prototypes, bench organisation and teaching aids. Intraoral use requires specific materials and processes.
A laser traces each layer cross-section to photopolymerise resin. Time depends on scan paths; accuracy depends on optics, material and process.
A micromirror (DMD) projector exposes the layer cross-section. Pixel size, optics, resin and layer separation all affect the result.
An LCD controls light transmission from LEDs. The “K” count describes the screen; it does not measure part accuracy by itself.
Low Force Display is the proprietary architecture in Formlabs Form 4/4B. It combines an LCD mask, illumination and release system; it is not a general category for Asiga or SprintRay DLP.
SLS uses a laser; MJF uses deposited agents and thermal energy. Both process polymer powder beds, predominantly in industrial workflows.
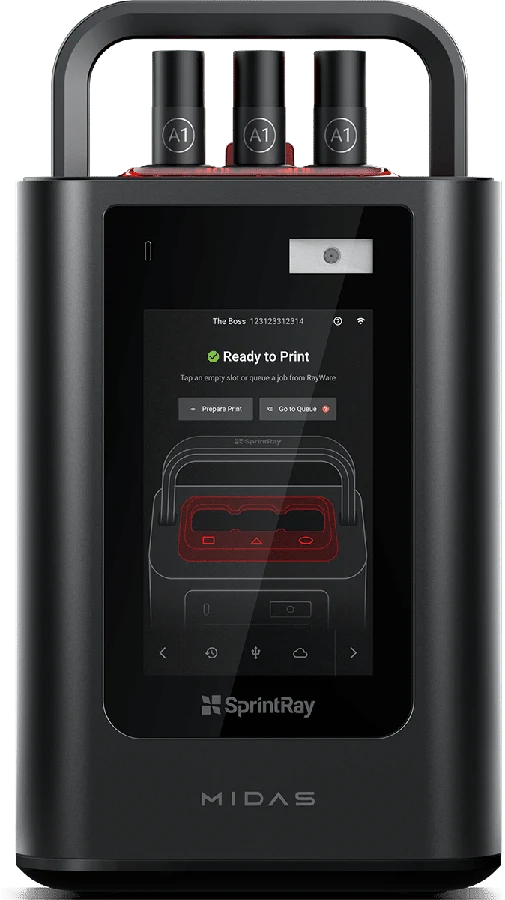
Digital Press Stereolithography is the proprietary process used by SprintRay Midas. Pressurised capsules enable processing of highly viscous, highly filled photopolymers; patterned light defines the layers.
Application: restorations within each material’s authorised indications. Results still depend on the capsule, printer and post-processing specified in the IFU. It is not ceramic pressing or sintering.
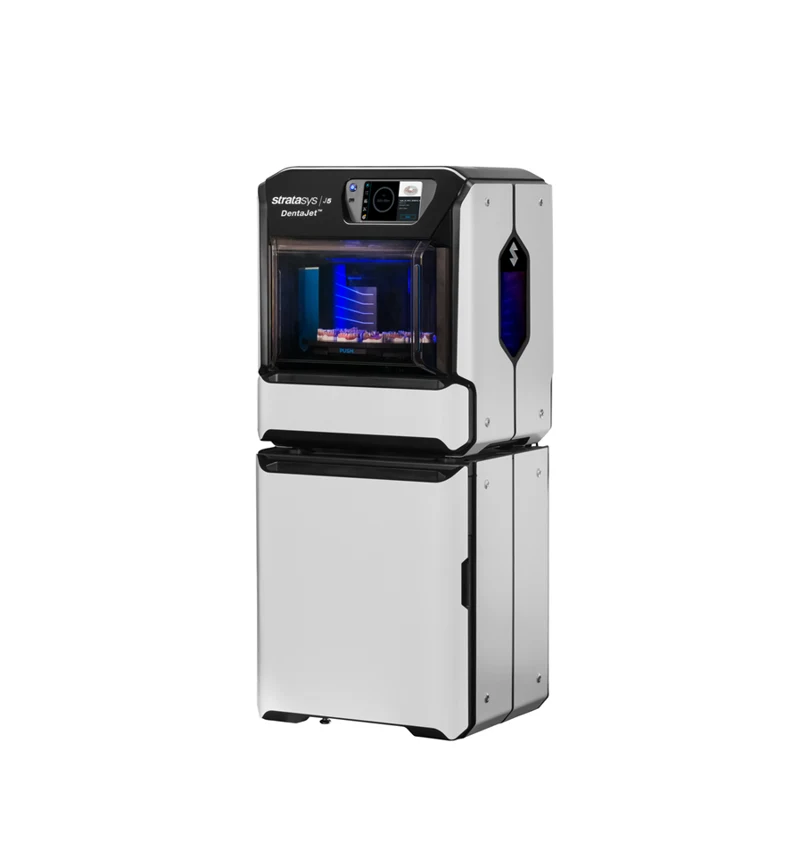
PolyJet is Stratasys material jetting technology. Printheads deposit photopolymer droplets that are UV-cured layer by layer. A separate support material is deposited and removed after printing.
Application: full-colour and multi-material models, depending on the equipment. The J5 DentaJet/TrueDent system can print dentures with base and teeth as one piece. Indications depend on the resin, IFU and region.
The design file is not the same file the printer actually runs.
| Type | Examples | Use | Limitation |
|---|---|---|---|
| Geometric mesh | STL | The most widespread format for models and CAD parts. | STL has no formal unit definition and carries no colour/texture. Check scale and mesh integrity. |
| Mesh with colour and texture | PLY, OBJ | Useful for colour scans, communication, face scanning and planning. | Not every slicer or CAD package uses that colour data clinically. |
| 3MF | 3D Manufacturing Format | Can preserve units, geometry and manufacturing metadata. | Extension support varies between programs. 3MF Consortium |
| Design or preparation project | DentalCAD, Blender (.blend), PreForm (.form) | Stores editable state in the relevant software; a preparation project is not necessarily parametric CAD. | Generally depends on the original software. |
| Sliced file | CTB, CB, PWMA/PWMX, Photon, PWS, ZIP, FORM and proprietary formats | Contains layer images, times, speeds, lift/retract values and printer metadata. | Not universal; a file sliced for one machine does not serve another. |
CHITUBOX, Lychee, Voxeldance Tango and Photon Workshop allow editing of exposure, layers, supports, compensations and, in many cases, speeds. They are useful for open systems, but require local validation.
PreForm, RayWare/SprintRay, Primeprint, Asiga Composer and similar ecosystems can work with validated libraries. Some allow fine editing; others restrict parameters to protect the protocol.
A part's performance depends on the whole chain, not on a single piece of equipment.
Decide whether the part will be a model, guide, occlusal device, provisional, long-term crown, prosthetic base or prototype.
Check the mesh, thickness, open borders, artefacts and scale before slicing.
Choose orientation, supports, layer height, exposure, lift distance, speed, compensations, and whether the part will be hollowed and vented.
Control resin, batch, agitation, temperature, vat, film, build plate, contamination and ambient light.
Remove liquid resin without saturating or weakening the part. Use solvent and time compatible with the instructions for use.
Increase the degree of conversion using the unit, duration and conditions in the IFU. This does not imply 100% monomer conversion.
Remove supports, adjust, polish and, where indicated, glaze and characterise without violating the material's indication.
Confirm fit, dimensional stability, absence of residual resin, batch documentation and traceability.
Naming follows CHITUBOX and similar slicers; closed systems may lock some of these settings.
| Parameter | What it controls | Impact | Common mistake |
|---|---|---|---|
| Layer Height | Height of each layer. | Smaller layers can improve vertical transitions, but increase time and do not always improve fit. | Using 25 µm without recalibrating exposure. |
| Exposure Time | Light time for normal layers. | Defines polymerisation, detail, layer strength and lateral dimension. | Under-exposing for speed, or over-exposing until margins swell. |
| Bottom Exposure | Light time for the bottom layers. | Increases adhesion to the build plate. | Excessive time causes elephant's foot; too little releases the part from the plate. |
| Bottom Layer Count | Number of layers using bottom exposure. | Affects initial adhesion and the stability of supported parts. | Excessive base on parts with critical regions close to the plate. |
| Transition Layers | Gradual transition between bottom and normal exposure. | Reduces cure discontinuity and the risk of delamination near the base. | Ignoring it when bottom exposure is far higher than normal exposure. |
| Rest Time | Independent waits before/after lift and after retract. | Allows resin to stabilise. | Removing a wait required by the resin profile. |
| Light-off Delay (legacy) | In CHITUBOX, includes lift, wait and retract. | Not the same as an independent wait. | Copying a Rest Time value; firmware interpretation can vary. |
| Lift Distance | How far the plate rises after each layer. | Must be enough to release the layer from the film and renew resin. | Short distance with a large or loose FEP film, or with viscous resin. |
| Lift Speed | Rising speed. | Influences peel force, delamination and support failure. | Rising too fast with a heavy part; some closed printers do not allow editing this. |
| Retract Speed | Return speed to the exposure position. | Affects turbulence, bubbles and resin stabilisation. | Aggressive retraction with filled resins. |
| Light PWM | Light-source duty cycle. | Modulates emitted intensity. | Treating PWM as image grayscale. |
| Picture Grayscale | Grayscale of the exposed image region. | Can change local light dose. | Changing the image without reassessing exposure. |
| Anti-aliasing | Smoothing of the visual steps in the sliced image. | May improve appearance, but does not correct geometry or poor exposure. | Confusing visual smoothing with dimensional accuracy. |
| Tolerance Compensation | Compensation of internal and external dimensions. | Useful for fits, models, analogues and threads, when validated. | Using compensation to mask a calibration error. |
On closed or validated systems, parameters such as lift speed, retract, PWM and cure time may not be editable. That is not necessarily a limitation; it can be part of the manufacturer's control and validation strategy.
Calibrating means finding a robust printing window, not merely getting a part to stick to the plate.
Check the IFU, wavelength, post-cure, washing, compatibility and the manufacturer's initial parameters.
Request a profile for your printer, slicer version, vat and film type, and post-curing unit.
Control temperature, agitation, batch, layer height, vat, film, plate, solvent and post-cure time.
XP2/Validation Matrix, R_E_R_F, Cones of Calibration and AmeraLabs Town help find the initial window.
Assess critical dimensions: thickness, pins, holes, fits, lines and walls. Appearance alone is not enough.
Validate on a model, guide, device, crown or structure equivalent to the intended indication.
Record printer, resin, batch, profile, temperature, orientation, washing, post-cure and result.
A new batch, colour, screen, FEP/PFA film, curing chamber or a temperature change justifies reassessment.
Most resin failures start with orientation, insufficient supports, islands or trapped resin.
Supports must stabilise the part against the film's peel force without marking critical areas. On crowns, avoid margins, internal surfaces and prime aesthetic zones. On occlusal devices, avoid the intaglio and functional surfaces wherever possible. On models, prefer bases, borders and areas with no clinical readout.
An island is a layer region that begins “in mid-air”, with no connection to the plate, to a support or to a previous layer. It cures against the film, becomes debris, leaves missing geometry and can puncture the FEP/PFA film or damage the screen. The fix is to change orientation or add a support before the island's first layer.
| Setting | Practical meaning | When to increase | When to reduce |
|---|---|---|---|
| Z Lift Height | Distance between the model's lowest point and the plate. | To improve access to supports and help resin drain. | When print time becomes unnecessarily long. |
| Light / Medium / Heavy | Presets for thickness, contact and density. | Large, heavy parts, viscous resin or a larger suction area. | Delicate parts or aesthetic areas, provided there are no islands. |
| Support Angle | Maximum angle between the surface tangent plane and the platform for automatic support generation. | When there are many unsupported regions or small islands. | When auto-support overshoots and marks critical areas. |
| Touch Tip Distance | Spacing between tips. Greater distance = lower density. | To space supports farther apart when stability is sufficient. | To increase density and reduce unsupported spans. |
| Contact Diameter / Tip Upper Diameter | Size of the contact area on the part. | When the part releases or islands fail. | When the support mark damages a critical surface. |
| Contact Depth | How deep the support tip penetrates the part. | To resist peel tension, especially on heavy parts. | When removal tears out material or leaves craters. |
| Upper / Lower Diameter | Diameters of the upper support segment. | When the support bends or breaks near the tip. | To reduce consumption and marking, if stability is maintained. |
| Middle Diameter / Angle | Thickness and inclination of the main pillar. | Heavy parts, large plates or rigid and viscous resins. | When there is excess material and removal becomes difficult. |
| Raft Shape / Raft Thickness | Anchoring base on the plate. | When the base detaches or the print fails at the start. | When adhesion is excessive and damages the plate or the part. |
Hollow models save resin and reduce mass, but they are only safe when the liquid resin can get out. If a hollow region is sealed, the part can stay wet inside even after washing and post-curing; that increases odour, resin exudation, biocompatibility failure, local softening, delayed cracking and bench contamination. Use an open base, drainage holes at low points and, where necessary, a second hole for air intake. Orientation and supports must allow drainage during both printing and washing.
Practical rule: before printing a hollow model, walk through every layer mentally. The resin has to get in, get out and be washed away. A cavity that does not drain is a design failure, not a cosmetic detail.
Post-processing is a manufacturing step. It is not just cleaning.
Removes surface liquid resin. Isopropyl alcohol, ethanol or manufacturer-specified solutions may be used. An excessive bath can alter surface, fit and strength. The protocol must follow the instructions for use.
An initial bath removes the excess; a second, cleaner one finishes the job. This reduces cross-contamination and tacky residue, especially on guides and internal geometries.
Increases the degree of conversion and can reduce residual monomers; it does not ensure complete conversion. It affects mechanical properties, colour and biological response. Follow the IFU: longer is not always better.
Heating can increase the mobility of radicals and monomers, favouring degree of conversion. In excess, it can distort, yellow or embrittle certain materials.
Oxygen can inhibit surface polymerisation. Some techniques use glycerine, nitrogen or specific chambers, but this depends on the resin and the manufacturer's validation.
Compatibility depends on the photoinitiators. Many open resins use 405 nm; some professional systems work at 385 nm. The resin must be compatible with the printer and with the curing unit.
In general, resins for dental 3D printing combine acrylate or methacrylate monomers and oligomers, photoinitiators, inhibitors, pigments and, in restorative materials, inorganic or ceramic fillers. Composition alters viscosity, translucency, radiopacity, strength, wear, sorption, solubility and the post-curing protocol.
Focused on dimensional stability, anatomical readability, low shrinkage and cost. They must not be used as intraoral biocompatible materials.
Must preserve dimension, accept the indicated sterilisation and maintain sleeve stability.
Usually use matrices with inorganic or ceramic filler for strength, wear resistance and aesthetics. They require adequate thickness, polishing and cementation.
May be rigid, flexible or thermo-reactive. Comfort, retention, wear and fracture depend heavily on the formulation.
Require dimensional stability, bonding between base and tooth, and resistance to ageing in a moist environment.
Liquid resin is a chemical hazard. Use suitable gloves, goggles, ventilation, bench protection and correct disposal. Clinical parts must be fully washed and post-cured per the instructions for use.
The real cost includes the printer, washing, curing, resin, support, maintenance, validation and learning time.
| System | Characteristic | Examples | Range | Trade-off |
|---|---|---|---|---|
| Open | More freedom. Allows different resins and slicers, but requires local calibration and documentation. | Elegoo Mars/Saturn, Anycubic Photon, Phrozen Sonic, UniFormation GKtwo, some Asiga configurations. | R$ 1,800–18,000+ | Steeper learning curve |
| Hybrid | Profiles with partial openness. Reduces trial and error while preserving some flexibility. | Formlabs Form 4B, Asiga, Ackuretta and workflows with validated libraries. | R$ 18,000–80,000+ | More manufacturer support |
| Closed | Process control. Less freedom, greater standardisation and a higher entry cost. | SprintRay, Dentsply Sirona Primeprint, Straumann/DMG/Saremco in validated ecosystems. | R$ 35,000–120,000+ | Profile validated by the system |
Approximate ranges for the Brazilian market. They can vary with exchange rate, taxes, warranty, wash-and-cure bundles, training, licensing and local support. They do not replace a formal quotation.
Values from public technical data sheets and studies. Do not compare them directly without accounting for the standard, orientation, printer, washing, post-cure and ageing.
| Material | Flexural strength | Flexural modulus | Composition and notes | Source and critical reading |
|---|---|---|---|---|
| Smart Print Bio Vitality — Smart Dent | 147 MPa | 5.49 GPa | Nano-hybrid resin; filler 58–59% by weight; Shore D >92; sorption 1.5 µg/mm³; radiopacity 1.048 mmAl. | Smart Dent · ficha técnicaStrength: ISO 4049, report cited by the manufacturer. Commercial data do not establish clinical longevity. |
| PriZma 3D Bio Crown Diamond — Makertech | 143 MPa | Not found | 52% silanised fillers per catalogue. Check the indication and protocol for each restoration type. | Makertech · catálogoModulus not found; not inferred from composition. |
| PriZma 3D Bio Crown — Makertech | Not found | Not found | Nano-hybrid composite resin with silanised ceramic and zirconia. | Makertech · catálogoConsult the formulation and system IFU/TDS. |
| Voxelprint Ceramic — FGM | Not found | Not found | ~60% by weight of inorganic glass-ceramic fillers; compatible with DLP/LCD at 385 or 405 nm; indicated for single prostheses on teeth and implants. | FGM · perfil técnicoThe document presents test graphs; approximate values were not extracted from bars. A print profile alone does not validate the entire clinical workflow. |
| BEGO VarseoSmile Crown Plus | 116–150 MPa | 4.09 GPa | Material for single restorations and prosthetic elements; performance depends on the validated system. | BEGO · Technical dataDeclared range depends on post-curing equipment; not a single-test mean. |
| Saremco print CROWNTEC | 155 MPa | 4.5 GPa | Resin for printed restorations; values depend on method and post-cure. | Saremco · TDS 04/2024Typical values; DIN EN ISO 4049. Specifications: >130 MPa and >4.0 GPa. |
| Formlabs Permanent Crown | ≈116 MPa | Not confirmed | Material from the validated Formlabs ecosystem; confirm the current IFU and a compatible printer. | Formlabs · IFU 2020Historical manufacturer IFU hosted by a distributor. The 4.09 GPa modulus was not confirmed in this source. |
| Material | Flexural strength | Flexural modulus | Other properties | Source and critical reading |
|---|---|---|---|---|
| KeyPrint KeySplint Soft | 44–47 MPa | 1.1–1.4 GPa | Elongation 100–120%; flexible, thermo-reactive material. | Keystone · TDS R5Strength and modulus: ASTM D790. The same TDS gives a different set of results under ISO 20795-2. |
| Voxelprint Splint Tough — FGM | Not found | Not found | Check properties for the formulation and commercial version. The ZIP’s toughness numbers were not reconfirmed in a primary data sheet in this revision. | FGM · VoxelprintNumerical data not reconfirmed. |
| Cosmos Splint — Yller | 88 MPa | 2.45 GPa | Values from the Cosmos Splint page; do not automatically assign them to the SLA variant. | Yller · Cosmos SplintISO 20795-1. Manufacturer-declared elastic modulus. |
| PriZma 3D Bio Splint — Makertech | Not found | Not found | Transparent biocompatible resin, indicated for retainers and occlusal devices; the catalogue includes a visual post-cure control. | Makertech · catálogoConsult the formulation and system IFU/TDS. |
| PriZma 3D Bio Splint Soft — Makertech | Not found | Not found | Flexible material; should not be compared directly with rigid splints. | Makertech · catálogoConsult the formulation and system IFU/TDS. |
| Formlabs Dental LT Comfort | ≈21 MPa | 0.643 GPa | Elongation: 33%; Shore D: 75. | Formlabs · material dataData from the manufacturer’s Form 3B, 100 µm, Form Wash and Form Cure protocol. |
| SprintRay NightGuard Firm | ≈119 MPa | 2.452 GPa | Resin for rigid occlusal devices. | SprintRay · NightGuard FirmManufacturer-declared values; check the protocol before comparing. |
| DETAX Freeprint splint 2.0 | Not confirmed | Not confirmed | Previous values removed pending a data sheet for the exact formulation. Do not transfer values between SLA/LCD versions or different materials. | Ivoclar · DETAX splint 2.0Indication documented; numerical data not reconfirmed. |
| Material | Flexural strength | Flexural modulus | Composition and notes | Source and critical reading |
|---|---|---|---|---|
| Cosmos Temp — Yller | Not confirmed | Not confirmed | A material for provisionals. Included for comparison, but it must not be treated as a resin for long-term crowns. | Yller / Dental SpeedDistributor reference inherited from the ZIP; values not reconfirmed in this revision. Provisional material. |
Strength and modulus values are not equivalent when measured under different standards, geometries, orientations, printers, cure times, atmospheres and ageing conditions. Where a figure does not exist in a public source, the table records its absence rather than estimating it.
Sources used for concepts, parameters, post-processing and public properties. Always confirm the current instructions for use.